 EN
Our Key Advantages
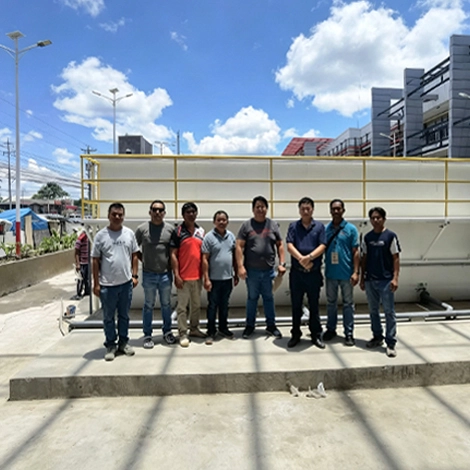
Successfully delivered wastewater treatment projects across multiple countries and industries. With an extensive project portfolio, we possess in‑depth knowledge of local environmental regulations and wastewater characteristics.
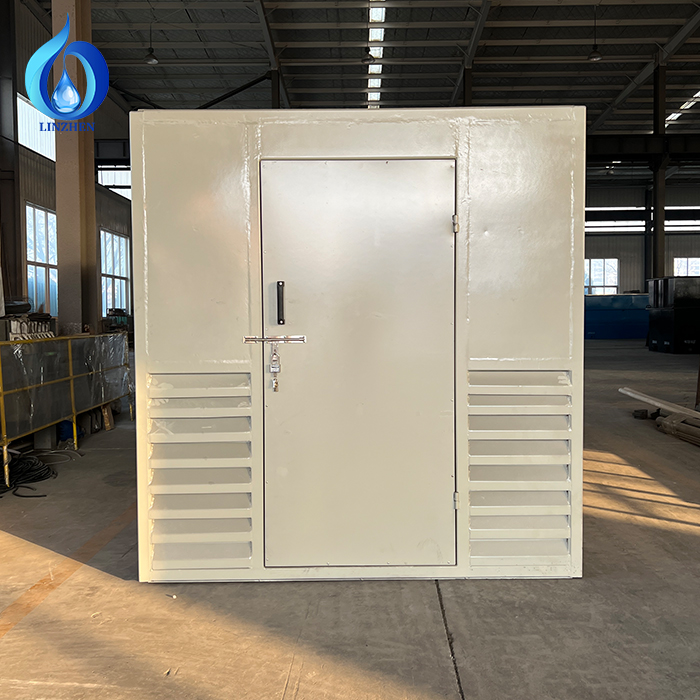
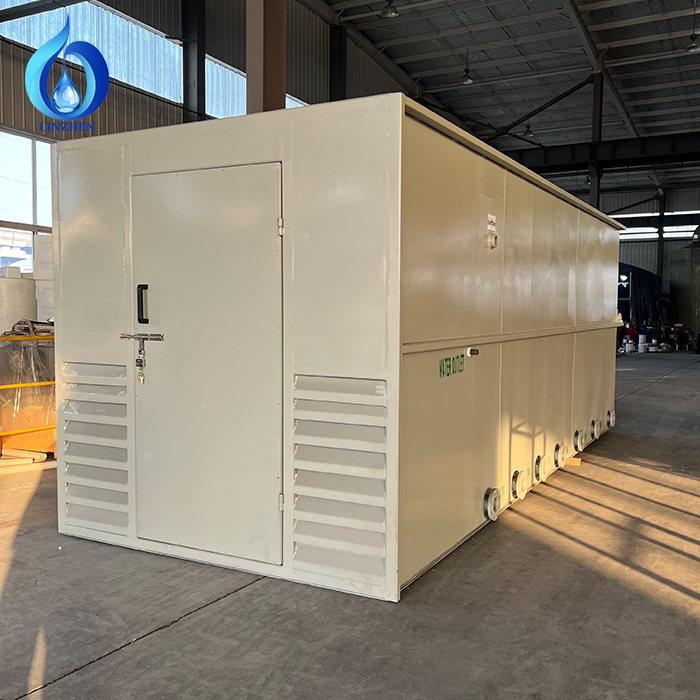
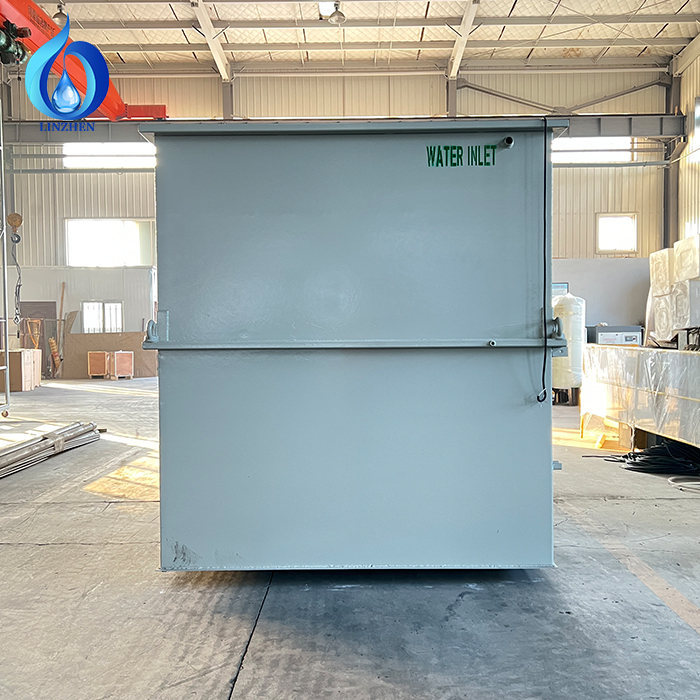
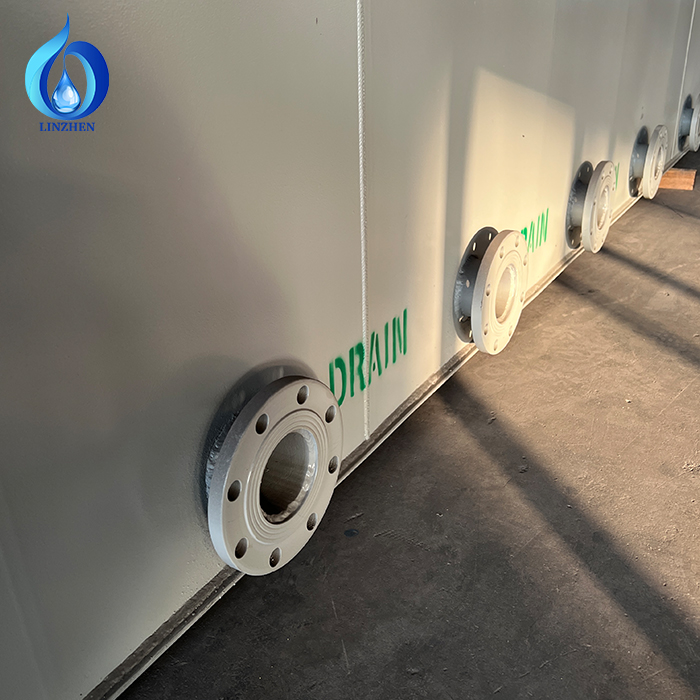
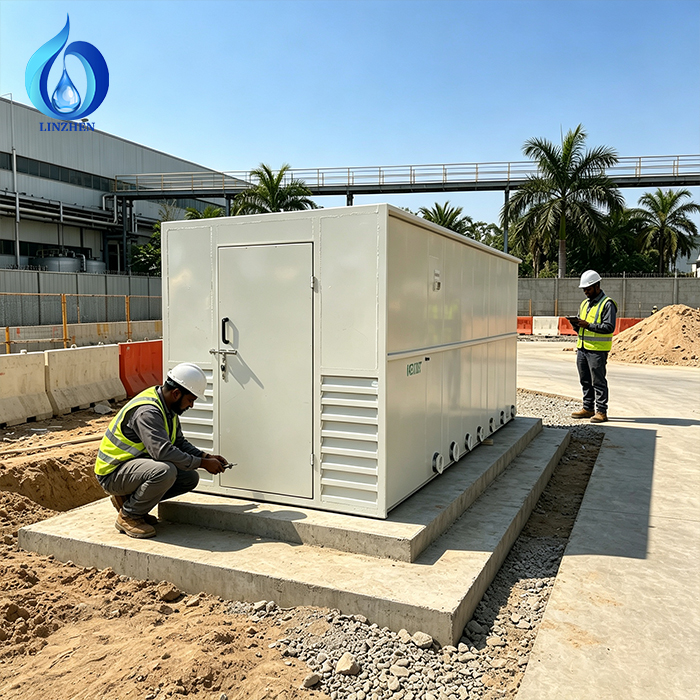
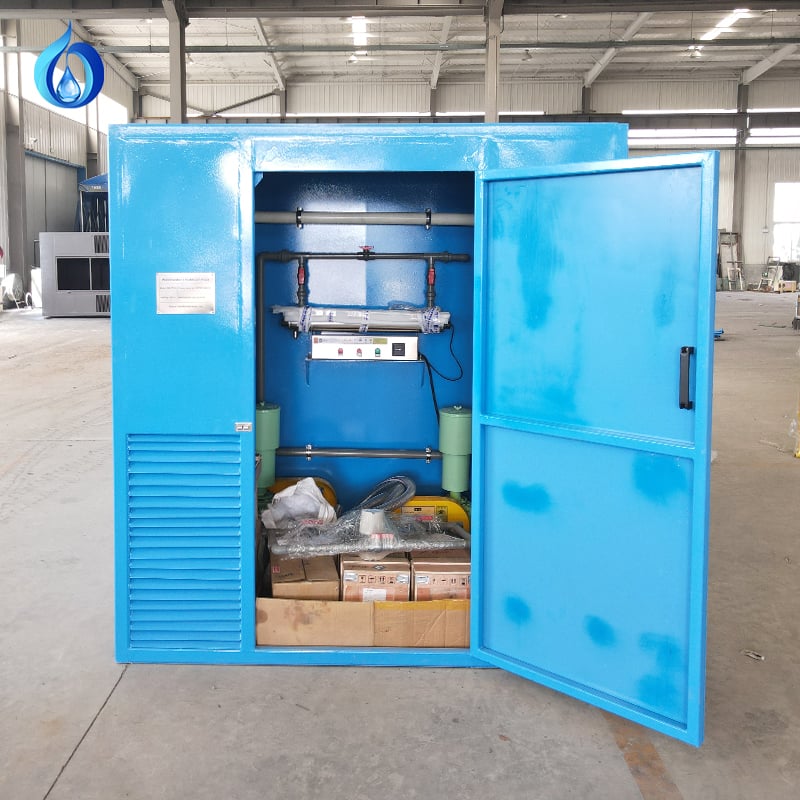
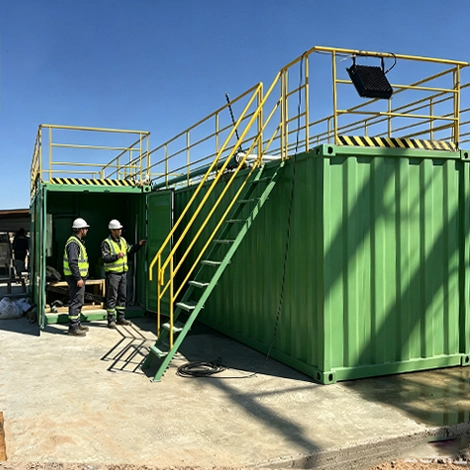
Compact membrane bioreactor systems combining biological treatment and membrane filtration to produce high-quality reclaimed water with minimal footprint and stable operation.
· Stable & High-standard Effluent Discharge Quality
· Low Operating Energy Consumption
· Double-layer Anti-corrosion Protection: Hot-dip Galvanization + Premium Heavy-duty Anti-corrosion Paint
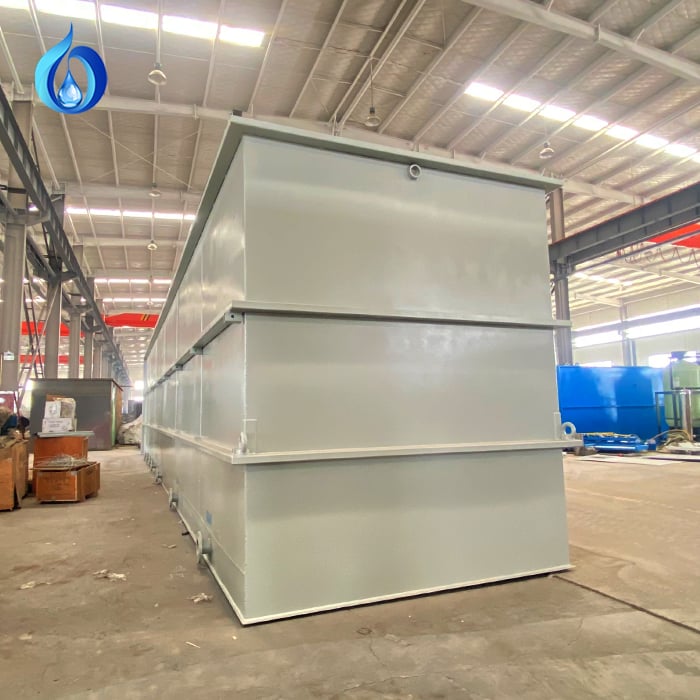
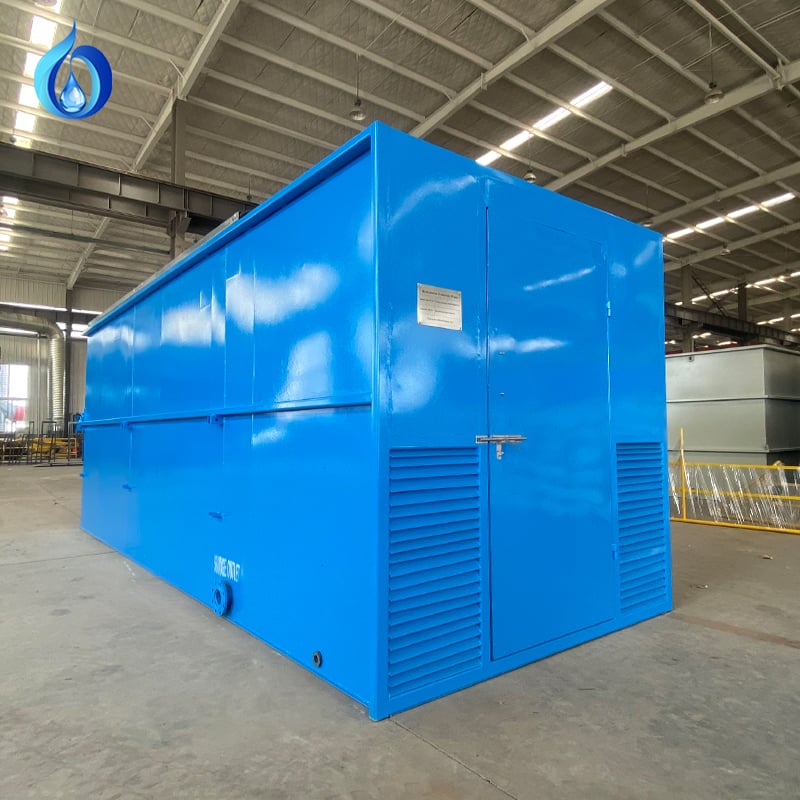
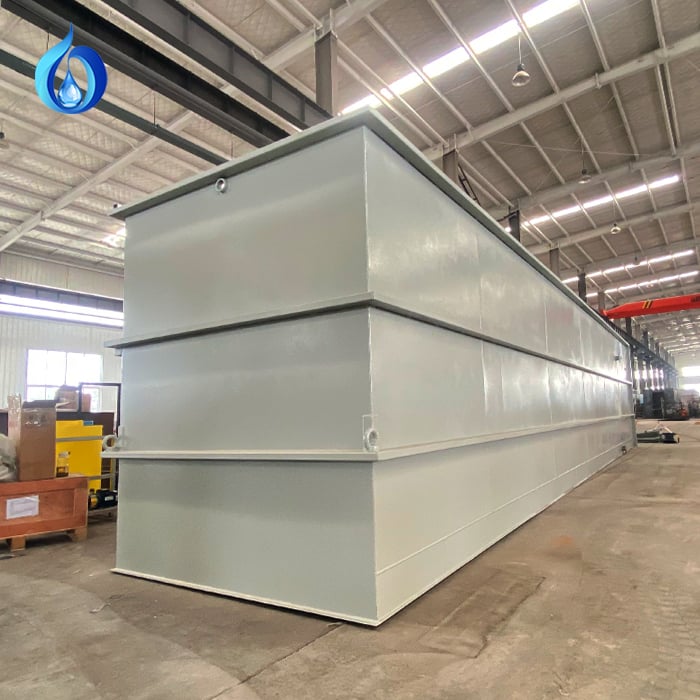
The MBR (Membrane Bioreactor) Wastewater Treatment System from Qingdao Linzhen Environment Project Co., Ltd. combines advanced biological treatment with membrane separation technology to deliver exceptional wastewater purification performance. By replacing traditional secondary clarifiers with high-precision membrane filtration, the system produces high-quality effluent suitable for discharge or water reuse while significantly reducing the overall footprint.
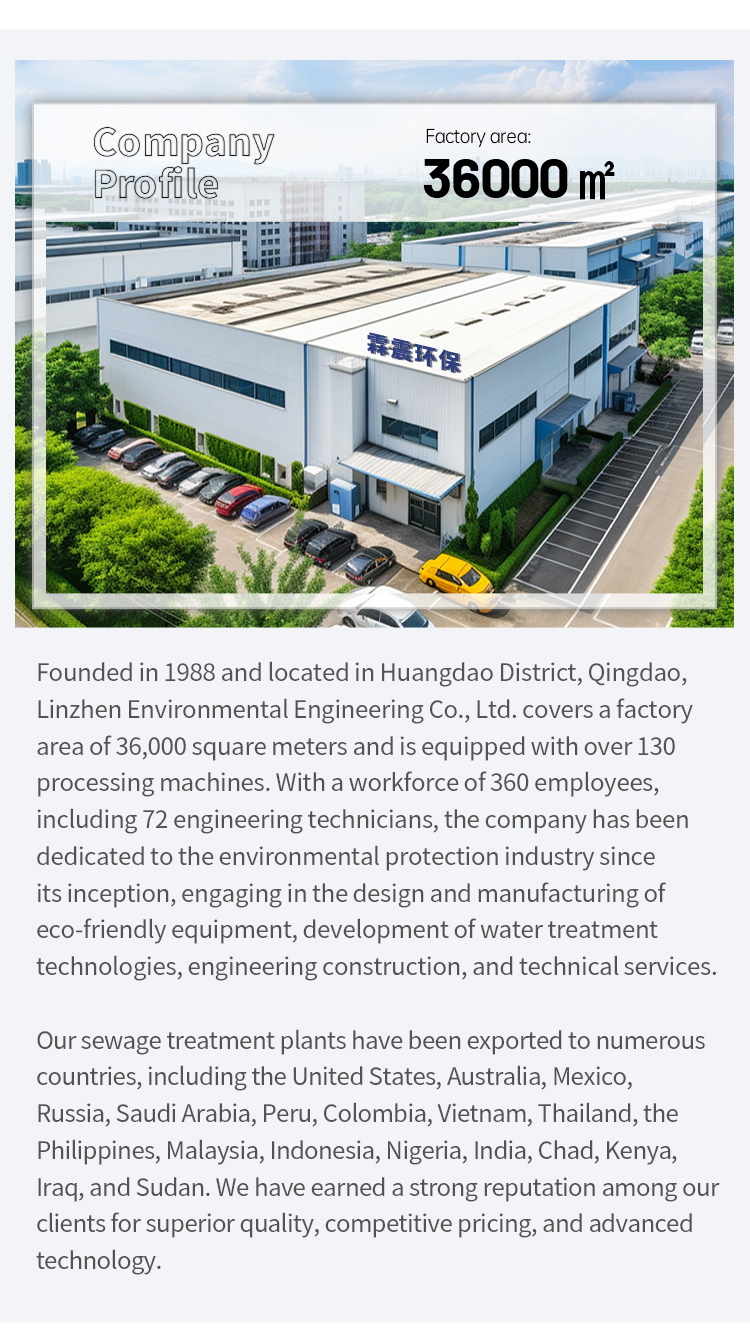
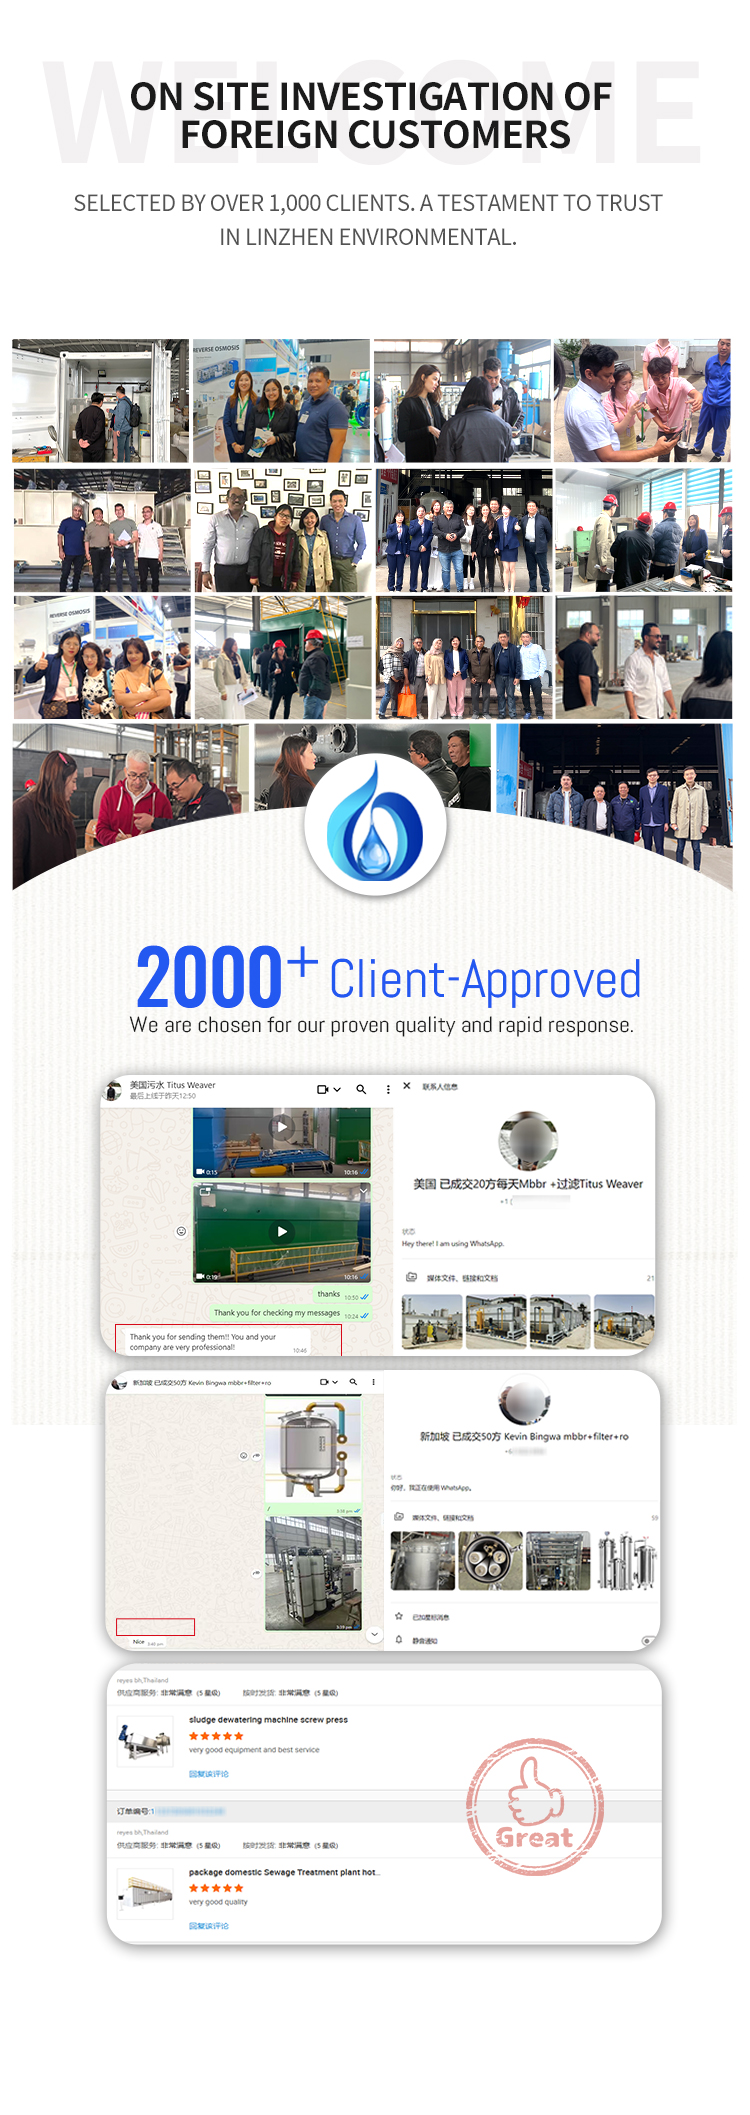
As a professional manufacturer of integrated sewage treatment equipment, industrial wastewater treatment systems, containerized wastewater treatment plants, and complete environmental protection solutions, Linzhen provides customized MBR systems for municipal, commercial, and industrial wastewater treatment projects worldwide. Our solutions have been exported to more than 50 countries across Asia, Europe, Africa, South America, and Oceania, serving EPC contractors, environmental engineering companies, municipal authorities, and industrial enterprises.
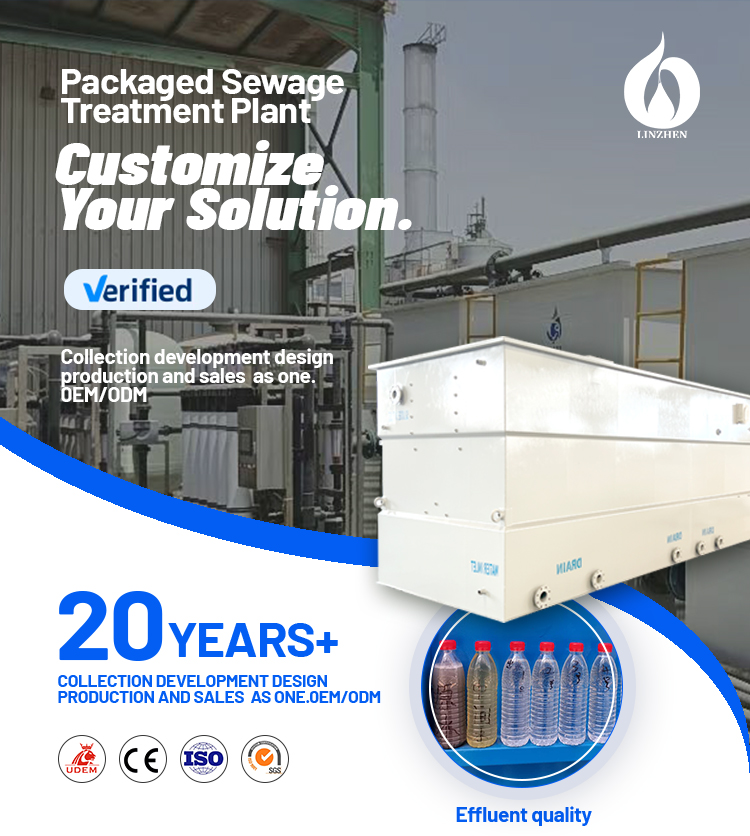
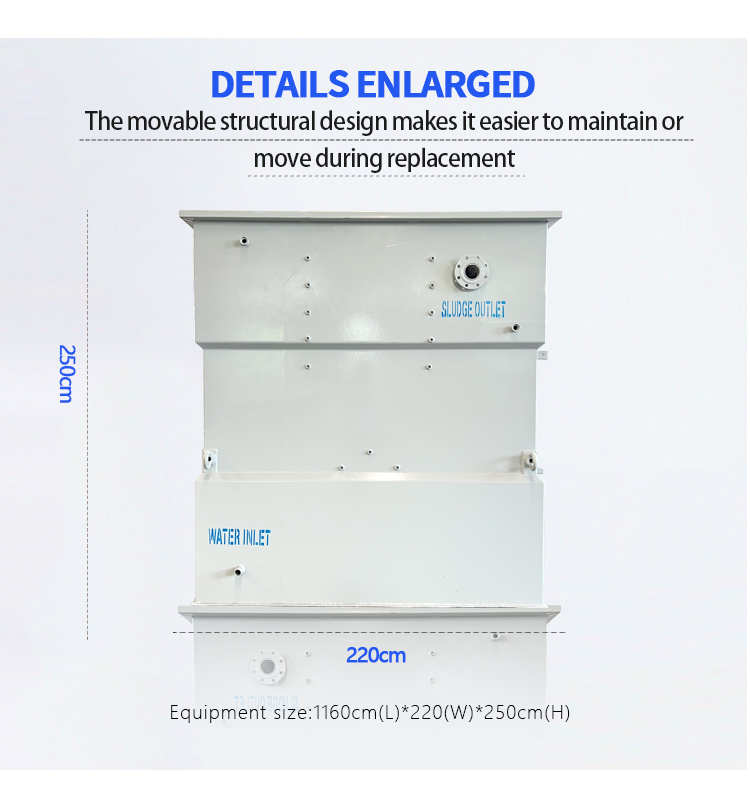
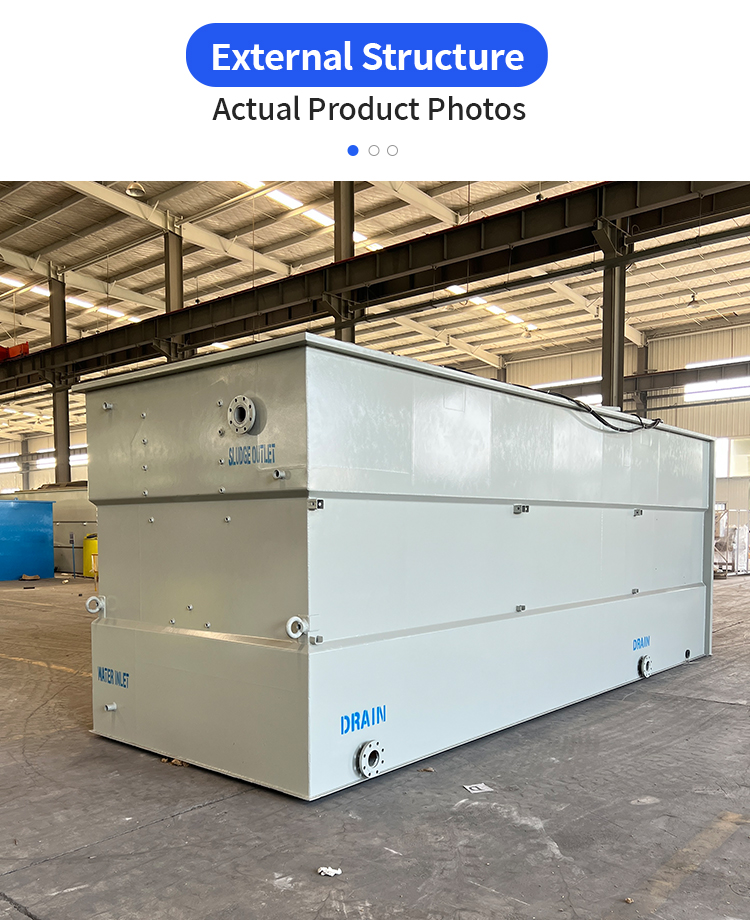
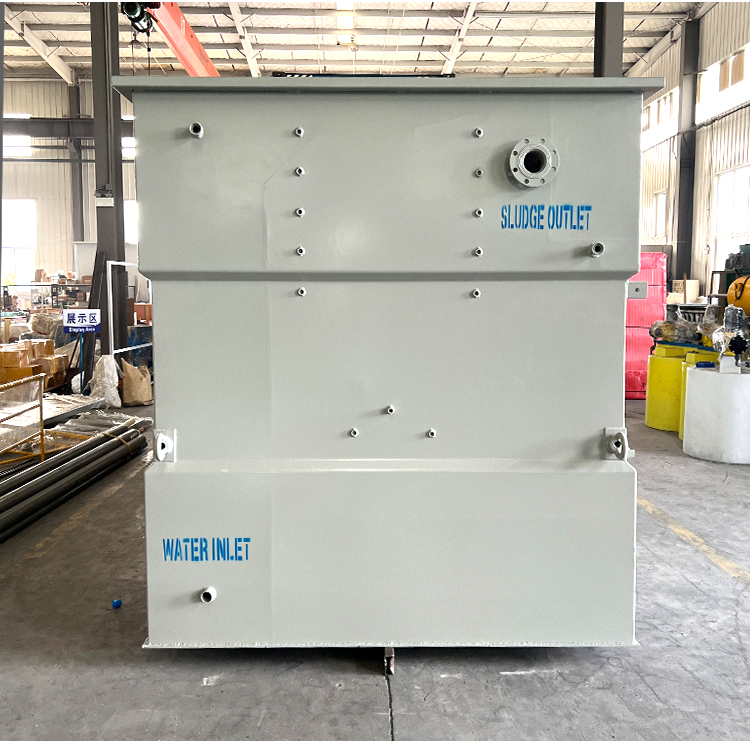
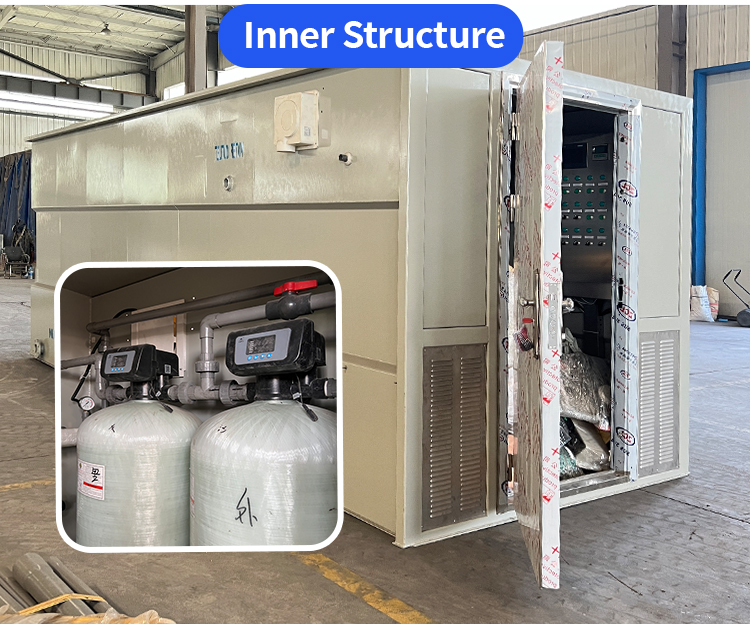
An MBR (Membrane Bioreactor) Wastewater Treatment System integrates activated sludge biological treatment with membrane filtration technology. Instead of conventional secondary clarifiers, ultrafiltration membranes separate treated water from activated sludge, producing superior effluent quality suitable for water reuse.
Compared with traditional wastewater treatment processes, MBR systems offer a significantly smaller footprint, higher biomass concentration, better removal efficiency, and stable operation under fluctuating influent conditions.
Linzhen designs and manufactures customized MBR wastewater treatment systems for municipal sewage, commercial wastewater, and industrial effluent treatment projects worldwide.
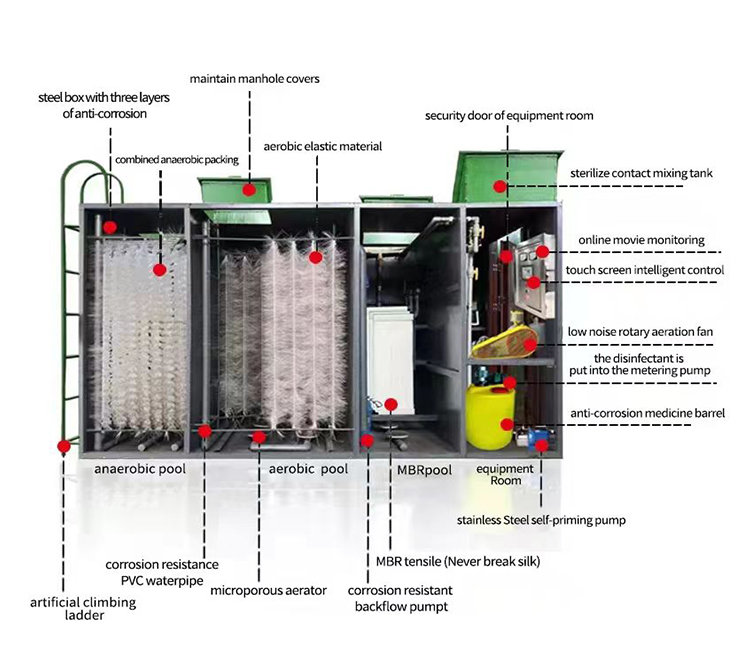
The Linzhen MBR system integrates multiple treatment stages into one efficient process, ensuring reliable wastewater purification and consistent discharge quality.
Incoming wastewater first passes through screening and grit removal equipment to eliminate large debris and protect downstream components.
The wastewater enters the biological reactor, where microorganisms metabolize biodegradable organic matter and convert pollutants into harmless substances.
Alternating anoxic and aerobic environments support biological denitrification and nitrification, effectively removing nitrogen compounds while reducing COD and BOD.
Instead of a traditional settling tank, ultrafiltration membrane modules separate activated sludge from treated water. The membranes retain suspended solids, bacteria, and most pathogens, producing high-quality effluent.
Optional UV or chemical disinfection further improves water quality, allowing the treated water to meet local discharge regulations or water reuse standards.
Full Automation
No manualintervention required,secure and stable.
Custom Services
Customized equipmentto solve your wastewatertreatment problems
Purification accuracy
Efficient purification withstable, Grade 1A effluentquality.
After-Sale
An efficient after-salesservice system with a30-person team
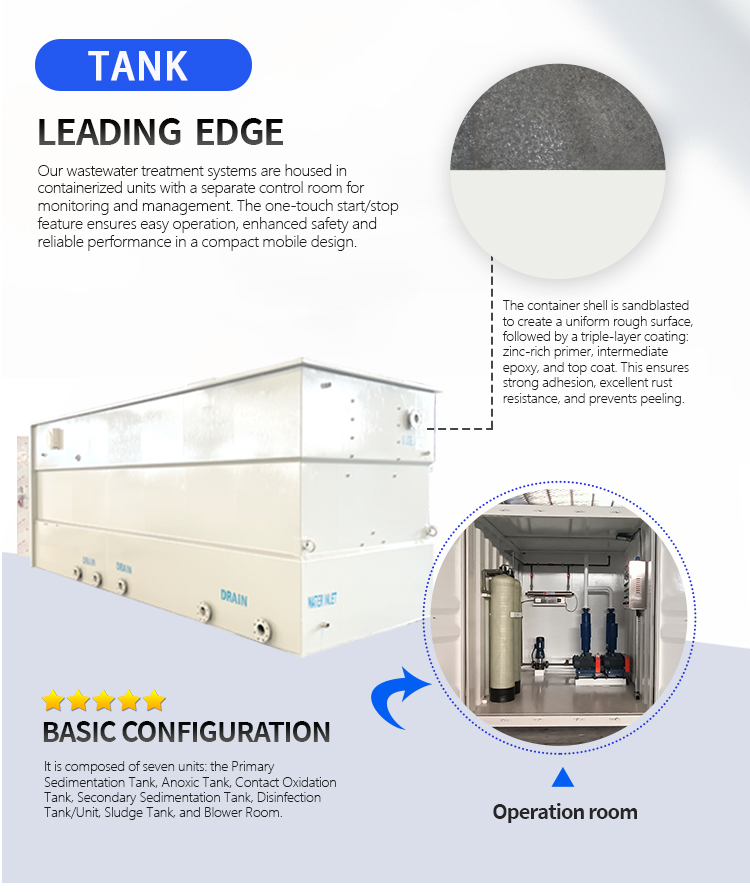
In treatment process, large bacteria and bacteria membrane update, adopt bio-logicalcarrier, improve the contact efficiency of micro- organism and pollutantmatter insewage; the whole treatment equipment produce anaerobic-anoxia-oxidation threekind of environment take turns function, improve purified waterability of differentkind of microbial population, intensify organism removal and nitrogen and phospho.rus removal function.
The working principle of the integrated sewage treatment equipment mainly relies onthe biological treatment method, which removes organic matter andother pollutantsin sewage through the metabolism of microorganisms. Thespecific process includespretreatment, biological treatment, anoxic and aerobic treatment, solid-liquid separa-tion, disinfection and discharge and other stages.
1.High Removal Efficiency
Excellent removal of COD, BOD, SS, ammonia nitrogen and pathogens.
2.Superior Effluent Quality
Produces reusable water meeting stringent discharge standards.
3.Compact Footprint
Requires up to 50% less installation space than conventional activated sludge systems.
4.No Secondary Clarifier Required
Membrane separation replaces traditional sedimentation tanks.
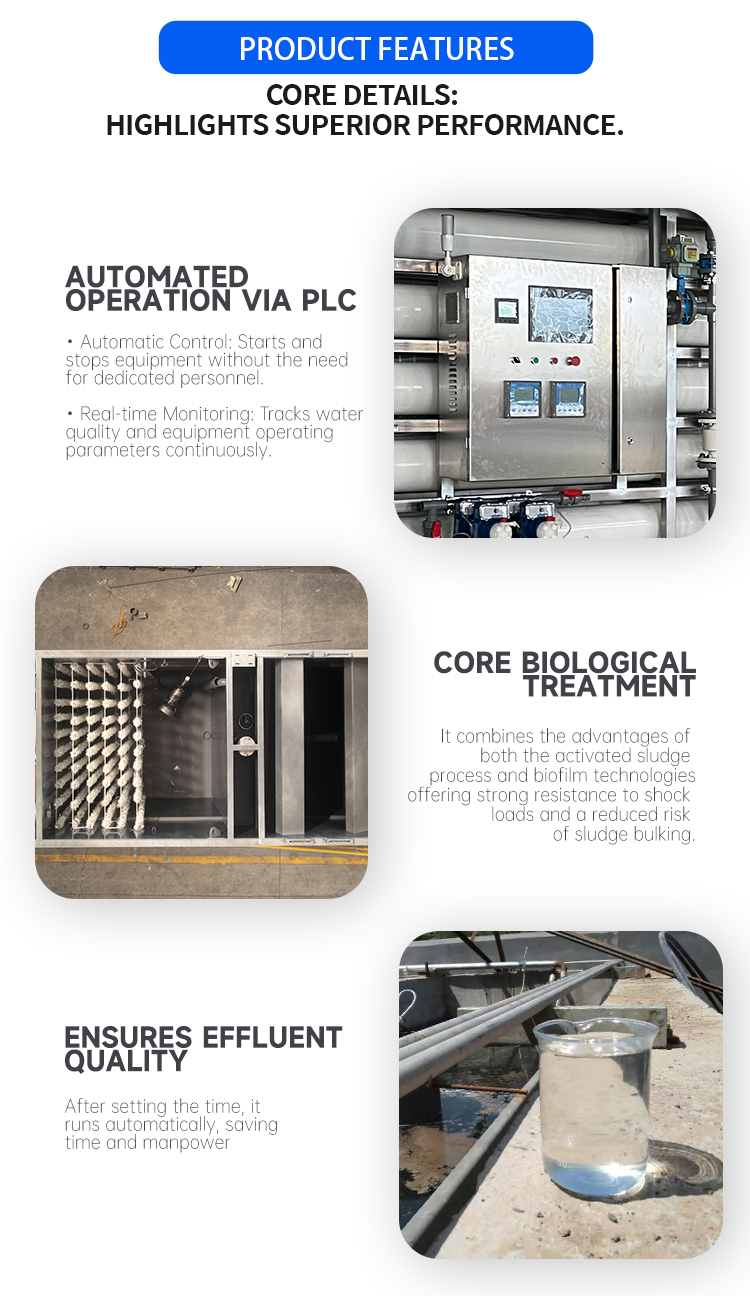
5.Fully Automatic Operation
PLC control with optional remote monitoring.
6.Easy Capacity Expansion
Modular design allows future expansion.
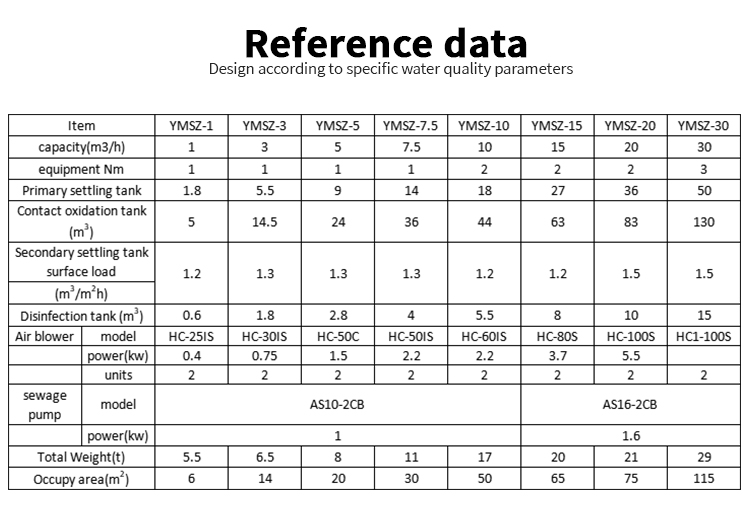
Key Attributes | |
Attribute Name |
Attribute Value |
productivity |
100m³/d |
Processing Type |
daf, mbr, mbbr, sbr, ao |
Voltage |
220v, 230v, 380v, 400v, 415v, 460v, 480v |
Power(W) |
5 kW |
core components |
Pump, Bearing, Motor, PLC, media, air blower, control pannel |
machinery test report |
Provided |
warranty |
1 Year |
video outgoing-inspection |
Provided |
weight (kg) |
4000 |
place of origin |
Shandong, China |
brand name |
LINZHEN |
MOQ |
1SET |
Material |
CEISO SABER COC |
Function |
Removing COD BOD NH-N SS Oil Grease Phosphorus |
Application |
industrial and domestic waste water |
Certification |
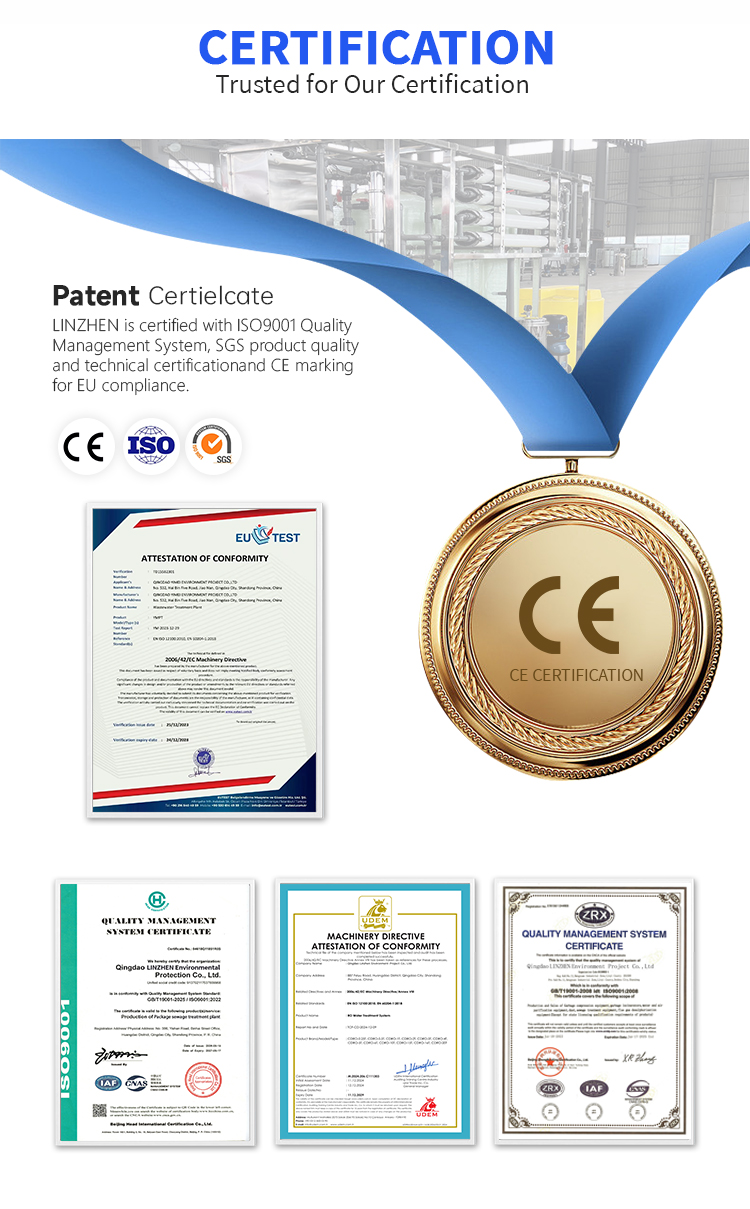
CEISO SABER COC |
Type |
PLC Automatic and Manual both |
Technology |
Dissolved Air Flotation, mbbr, mbr |
keyword |
Package Sewage Treatment Plant |
After Warranty Service |
1 Year |
Parameter |
Influent |
Effluent |
COD |
300–1000 |
<50 mg/L |
BOD |
150–500 |
<10 mg/L |
SS |
150–300 |
<5 mg/L |
NH₃-N |
20–60 |
<5 mg/L |
TN |
Customized |
Customized |
The system is widely applied in municipal sewage treatment plants, residential communities, hotels, hospitals, schools, office buildings, commercial complexes, and tourism facilities where stable wastewater treatment and water reuse are required. It is also an excellent solution for remote villages, construction camps, mining sites, and other decentralized wastewater treatment projects with limited installation space.
For industrial wastewater treatment, the MBR system is suitable for food and beverage processing, dairy factories, breweries, slaughterhouses, textile manufacturing, pharmaceutical production, chemical processing, and many other industries. The treated water can be discharged in accordance with local environmental standards or further reused for irrigation, toilet flushing, equipment cleaning, cooling water, and other non-potable applications.
· UV Disinfection
· Chlorine Dosing
· Sludge Dewatering
· Online Monitoring
· Odor Control
· Solar Power Integration
Compact membrane bioreactor systems combining biological treatment and membrane filtration to produce high-quality reclaimed water with minimal footprint and stable operation.
· Stable & High-standard Effluent Discharge Quality
· Low Operating Energy Consumption
· Double-layer Anti-corrosion Protection: Hot-dip Galvanization + Premium Heavy-duty Anti-corrosion Paint

Successfully delivered wastewater treatment projects across multiple countries and industries. With an extensive project portfolio, we possess in‑depth knowledge of local environmental regulations and wastewater characteristics.

Providing customized wastewater treatment solutions based on wastewater quality, operational requirements, discharge standards, and site conditions.


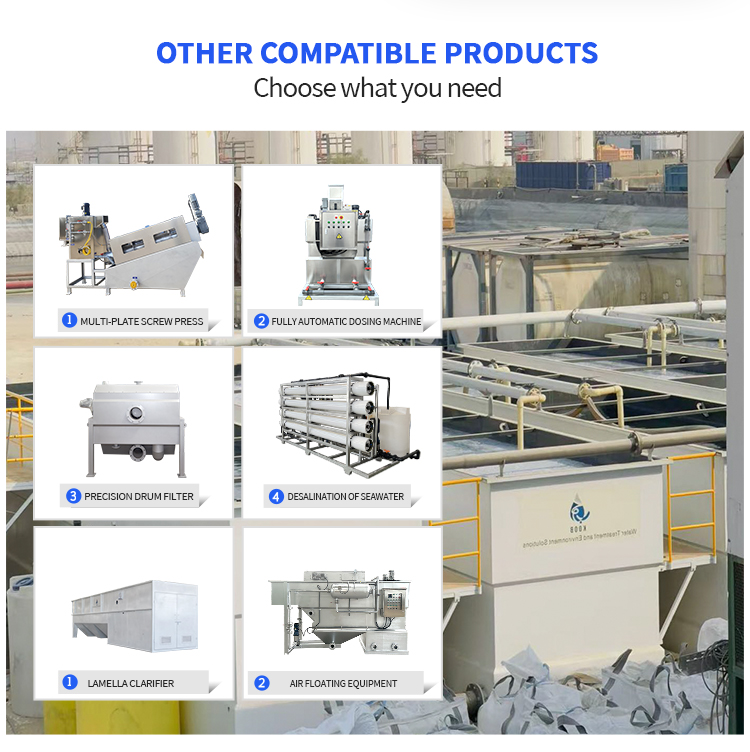
Specializing in proven treatment processes including MBR, MBBR, A/O, A²/O, RO, DAF, and Lamella Clarifier for various wastewater treatment applications.

Key components such as pumps, blowers, membrane modules, and electrical control systems are sourced from world‑renowned brands to ensure long-term stable operation.

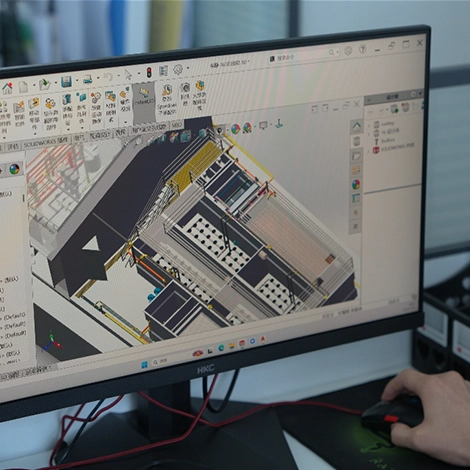
Providing comprehensive one-stop technical support covering solution design, equipment installation, commissioning, operator training, and after-sales service.
Tel
Address
Workshop 6, No. 88 Yueyahe Road, Huangdao District, Qingdao City, Shandong Province, China

 Case Studies
 Technical Downloads
 Engineering
 FAQ